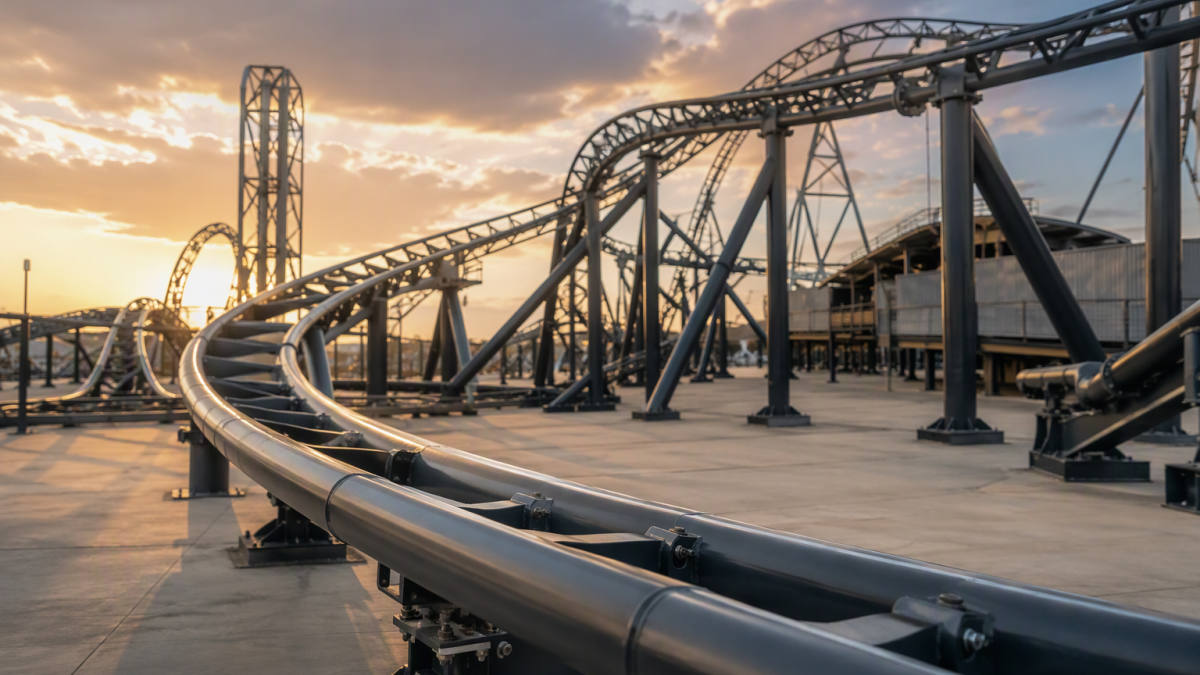
Before shipment, verify that coaster track segments meet the design geometry within agreed tolerances, that weld and coating integrity are documented, and that interface points (flanges, splices, supports) align within specified limits. Require a dimensional inspection report (CMM or total station) for every segment, confirm that tolerance stack-ups at joints are within allowable deviations, and ensure all non-destructive testing (NDT) and traceability records are complete. Ship only after a pre-shipment review confirms that track meets the project’s approved tolerances and that any deviations are dispositioned.
Why track tolerances matter more than most procurement teams expect
Roller coaster track is a dynamic structure. Small fabrication deviations can amplify into noticeable vibration, excessive wear on wheels and bearings, and uncomfortable or unsafe ride characteristics. Tolerances are not arbitrary; they are derived from the ride’s dynamic envelope, wheel assembly clearances, and the need for smooth transitions. For procurement, the key is to ensure that the fabricator’s tolerances are explicitly defined, measurable, and verified before shipment. This avoids costly site modifications, delays, and disputes.
Track fabrication tolerances typically cover: segment length, cross-section profile (gauge, twist, camber), longitudinal curvature (vertical and horizontal), weld quality and distortion, hole patterns for connections, and surface finish. Each must be checked against approved shop drawings and the project’s technical specification. Standards such as ASTM F2291 or EN 13814 may apply, but their specific acceptance criteria should be confirmed per project.
Key dimensional checks before shipment
Dimensional verification is the core of pre-shipment inspection. The fabricator should provide a detailed inspection plan that identifies critical-to-quality (CTQ) characteristics. For each track segment, the following should be measured and recorded:
- Overall length and end-to-end dimensions: Verify against design, accounting for thermal expansion if segments are fabricated outdoors.
- Track gauge and cross-level: Measure at multiple stations along the segment; deviations can cause wheel lift or excessive lateral forces.
- Vertical and horizontal curvature: Use a total station or laser tracker to compare actual geometry to the theoretical curve. Check for smooth transitions, especially at splices.
- Twist and camber: Particularly important for inversions and banked turns; excessive twist can cause roll misalignment.
- Flange and splice interface dimensions: Bolt hole patterns, flange flatness, and hole diameters must match mating segments within tolerance to ensure proper fit-up on site.
- Support bracket locations: Verify positions and orientations relative to the track centerline; misalignment can cause installation delays.
All measurements should be traceable to calibrated instruments, and results recorded in an inspection report. Any out-of-tolerance condition must be dispositioned (rework, repair, or accept with concession) before shipment.
Weld quality and distortion control
Welds are both structural and geometric. Poor weld quality can lead to fatigue cracking, while weld distortion can throw track geometry out of tolerance. Before shipment, verify:
- Weld procedure specifications (WPS) and welder qualifications: Confirm that welds were made according to approved WPS and by qualified welders.
- Non-destructive testing (NDT): Typically visual and dye penetrant or magnetic particle testing for surface defects; ultrasonic or radiographic testing for critical full-penetration welds. The extent and acceptance criteria should be defined in the project specification.
- Distortion measurement: After welding, measure straightness and profile again. If distortion exceeds allowance, straightening may be required, followed by stress relief if specified.
- Weld maps and traceability: Each weld should be identifiable and linked to its inspection record.
Hot-dip galvanizing after fabrication can introduce additional distortion if not controlled. If galvanizing is specified, confirm that the fabricator has procedures to manage heat distortion and that post-galvanizing dimensions are still within tolerance.
Coating, corrosion protection, and surface finish
Track segments are often hot-dip galvanized for corrosion resistance. Before shipment, check:
- Coating thickness: Measured at multiple points per segment; should meet the project specification.
- Coating adhesion and appearance: No bare spots, runs, or excessive roughness that could affect wheel contact.
- Threaded holes and machined surfaces: Must be masked or cleaned after galvanizing to ensure proper fit of bolts and bearings.
- Surface finish on running surfaces: If the track has a running surface (e.g., for polyurethane wheels), verify smoothness and absence of defects that could cause vibration.
Any paint or topcoat should be applied according to the specification, with proper surface preparation and curing. Documentation of coating system and dry film thickness readings should be included in the shipment package.
Pre-shipment checklist and documentation package
Use the following checklist to structure your pre-shipment review. The documentation package should be complete and reviewed before authorizing shipment.
| Check | Description | Documentation Required |
|---|---|---|
| Dimensional inspection | Verify segment geometry, gauge, curvature, twist, and interface dimensions against approved drawings. | Inspection report with measurements and pass/fail status. |
| Weld quality | Confirm WPS, welder qualifications, and NDT results. | Weld map, NDT reports, welder certificates. |
| Coating | Check galvanizing/paint thickness and adhesion. | Coating thickness readings, adhesion test results. |
| Interface fit-up | Pre-assemble or check mating flanges and bolt holes. | Fit-up report or photos. |
| Traceability | Link materials and welds to records. | Material certificates, heat numbers, weld traceability. |
| Packaging and protection | Ensure segments are protected for transport. | Packing list and photos. |
This checklist should be adapted to the specific project requirements. For complex rides, consider a third-party inspection at the fabricator’s works. ZhipaoRides, for example, can provide detailed inspection reports and remote diagnostics support to help buyers verify tolerances before shipment. Their manufacturing base in Xingtai, Hebei, includes capabilities for large-scale track fabrication and hot-dip galvanizing.
Common pitfalls and how to avoid them
Even with a checklist, issues can arise. Common pitfalls include:
- Assuming shop tolerances are sufficient: Always confirm that the fabricator’s standard tolerances align with the ride’s dynamic requirements. For high-speed or inverted coasters, tighter tolerances may be needed.
- Neglecting thermal effects: Segments fabricated outdoors can change dimensions significantly with temperature. Ensure measurements are taken at a consistent temperature or corrected.
- Incomplete documentation: Missing NDT reports or material certificates can delay shipment or cause acceptance issues.
- Poor communication of interface requirements: Flange and bolt hole patterns must be clearly defined and verified; otherwise, site assembly becomes a nightmare.
- Ignoring packaging: Inadequate protection can lead to damage during transport, undoing all previous quality work.
To mitigate these, establish a clear inspection and test plan (ITP) at the contract stage, hold a pre-shipment meeting, and require the fabricator to notify you of any deviations before shipment. For projects involving roller coasters with up to 11 inversions or launched/suspended types, consider engaging an experienced inspector. You can learn more about ZhipaoRides’ product range at /products.
Conclusion
Pre-shipment verification of track fabrication tolerances is a critical step in ensuring a roller coaster’s successful installation and operation. By focusing on dimensional accuracy, weld integrity, coating quality, and documentation, buyers can avoid costly site modifications and delays. Remember that standards and acceptance criteria should be confirmed per project, and always tailor the inspection plan to the specific ride’s requirements. With careful oversight, you can ensure that track segments arrive at the site ready for assembly and that the ride performs as designed.